English
 русский
 Français
 Español
 Português
 Deutsch
 عربى
 Türk
High Speed Spooler and Coiler: Selection Guide for Wire Rope Processing
Content
- 1 What a High Speed Spooler and Coiler Does in Wire Rope Production
- 2 Key Specifications to Compare Before Buying
- 3 How Spooling Speed Affects Downstream Swaging and Annealing
- 4 Common Operating Problems and How to Avoid Them
- 5 Matching a Spooler and Coiler with Your Existing Press and Annealing Line
- 6 Visual Comparison: Spooling Speed vs. Wire Rope Diameter
- 7 Maintenance and Safety Practices for High Speed Winding
- 8 FAQ
When you are setting up a wire rope processing line, the high speed spooler and coiler often becomes the bottleneck or the hero. A spooler that runs smoothly at 200 meters per minute can keep your hydraulic press and annealing machine fed without constant stops. But if tension control is off by even a few percent, you get loose wraps, birdnesting, or uneven payout that ruins the next swaging operation.
The conclusion: choose a spooler and coiler based on line speed, tension range, drum diameter, and how well it integrates with your existing press and taper/annealing equipment. Do not buy on price alone. The right unit will pay back through less downtime and fewer scrapped assemblies.
What a High Speed Spooler and Coiler Does in Wire Rope Production
A high speed spooler and coiler handles three jobs: paying wire rope off a supply reel, winding it onto a take-up drum at controlled tension, and sometimes rewinding for storage or shipping. In a wire rope shop, you will see it before or after the hydraulic press, and often next to an annealing machine.
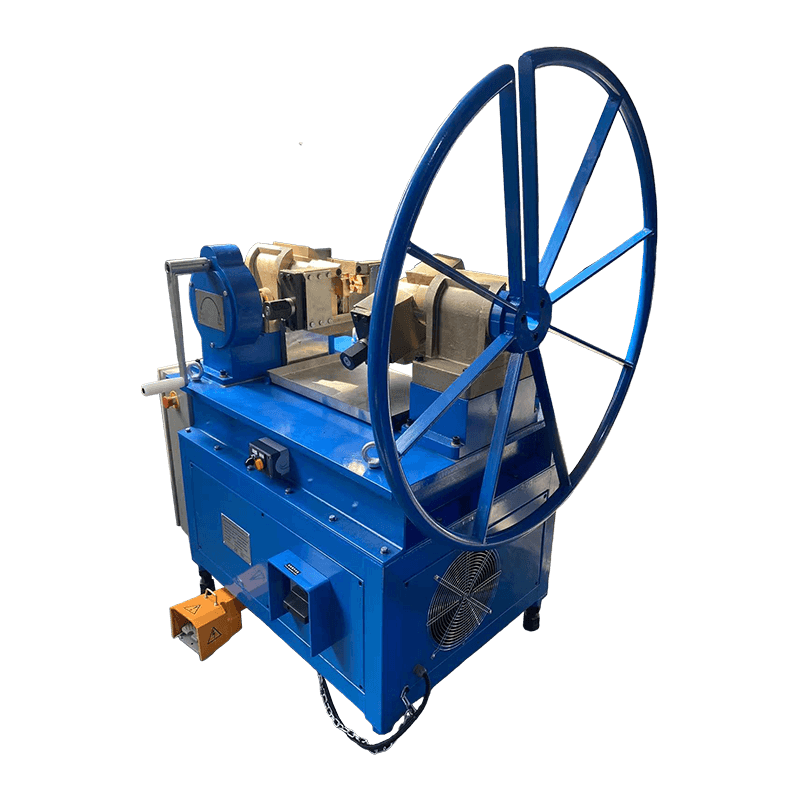
The XT1600 wire rope reeling machine from Jiangsu Xingtai is a good example. It is designed for continuous reeling and unreeling, with a motorized drum and adjustable tension. Unlike a simple winder, a spooler for wire rope must avoid crushing the strand, keep the lay direction consistent, and allow quick drum changes.
Core functions that affect your daily output
- Constant tension: Prevents loose layers that collapse when the press pulls wire.
- Speed matching: The spooler must accelerate and decelerate in step with the press cycle.
- Drum handling: Quick-lock arbors reduce changeover time from minutes to seconds.
If your spooler cannot hold tension within ±5%, you will see variations in the finished rope assembly length. That means rework, wasted ferrules, and unhappy customers.
Key Specifications to Compare Before Buying
When you request quotes from a manufacturer or supplier, ask for a specification table. The numbers below matter more than the paint color. Use this comparison as a checklist.
| Specification | Entry Level | Mid Range | High Speed / Heavy Duty |
|---|---|---|---|
| Line speed (m/min) | 30–60 | 60–120 | 120–250+ |
| Tension control | Manual brake | Pneumatic or magnetic | Servo / closed-loop |
| Max drum weight (kg) | 500 | 1,500 | 3,000+ |
| Wire rope diameter (mm) | 4–12 | 8–24 | 12–48 |
| Integration | Stand-alone | With press or annealer | Full line PLC |
Notice that high speed does not only mean a faster motor. It requires a stronger frame, better bearings, and a tension system that can respond in milliseconds. If you buy a cheap high-speed unit without closed-loop tension, you will fight vibration and uneven wraps every shift.
How Spooling Speed Affects Downstream Swaging and Annealing
Your hydraulic press and annealing machine do not work in isolation. The spooler feeds them. If the spooler delivers wire at a jerky pace, the press will produce inconsistent crimps. If the annealer pulls wire faster than the spooler can pay off, you get tension spikes that stretch the rope.
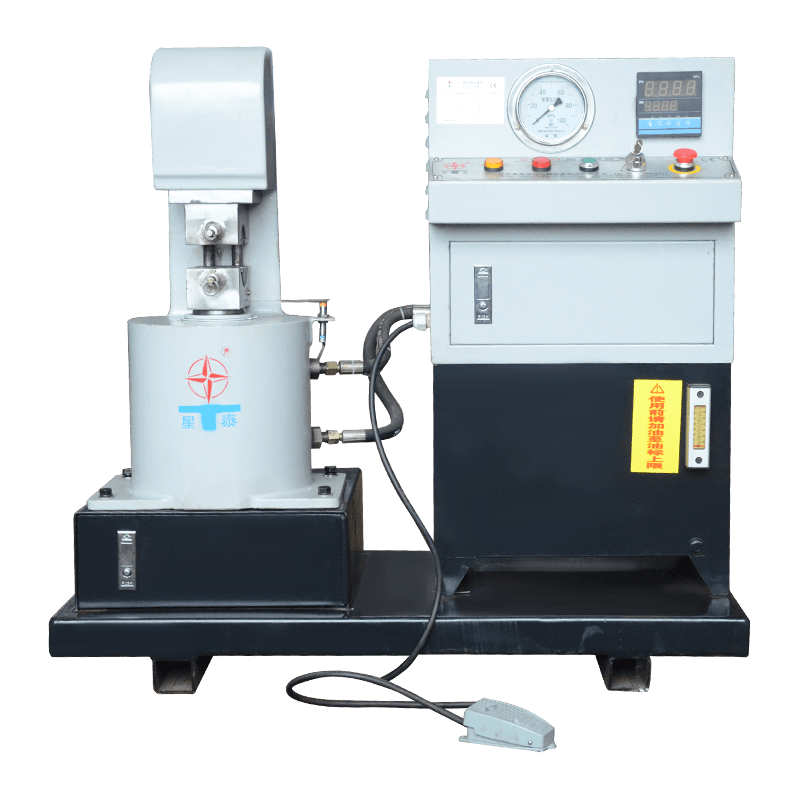
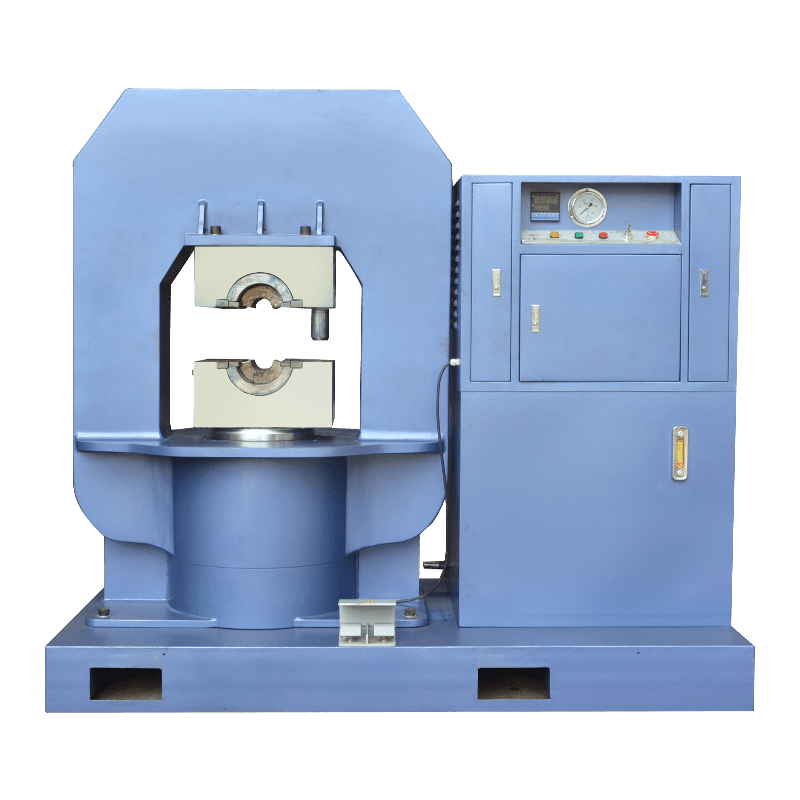
For example, a GT1000 hydraulic wire rope sleeve pressing machine can cycle every few seconds. The spooler must be able to start and stop without overshooting. That is why many shops pair a high speed coiler with a dancer roller or accumulation loop. The loop absorbs speed differences between the spooler and the press.
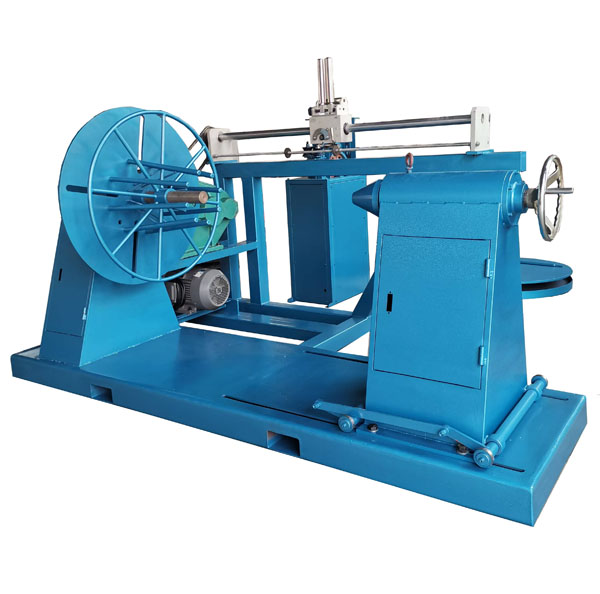 XT-1600 Wire Rope Reeling MachinesWire Rope Winding Machine is a device used for winding or unwinding ropes. It enables the mechanical operation of coiling or releasing steel wire ropes, improving work...View Product →
XT1600 is built for this kind of buffering. Its variable frequency drive lets you set a base speed and let the dancer control fine adjustments. When you later add an annealing machine, the same spooler can handle both payout and take-up if you choose the right drum size.
Common Operating Problems and How to Avoid Them
Even a well-built spooler can misbehave if you ignore the basics. Here are the four issues we hear about most from wire rope manufacturers.
- Birdnesting on the supply reel: Usually caused by too little back tension. Increase the brake or use a motorized payoff.
- Loose wraps on the take-up drum: Often a sign that the traverse guide is too slow or the tension is too low. Adjust the pitch and tension.
- Wire rope twisting: Happens when the spooler pulls at an angle. Align the spooler with the press and annealer within 1 degree.
- Drum slip: Worn arbors or inadequate clamping. Check the locking mechanism every 500 hours.
Preventive maintenance is cheaper than emergency repairs. Keep the spooler’s bearings greased, check the tension sensor calibration monthly, and replace worn guide rollers before they cut into the rope.
Matching a Spooler and Coiler with Your Existing Press and Annealing Line
You may already own a hydraulic press and an annealing machine. Adding a high speed spooler and coiler should not require replacing everything. The key is interface compatibility: signal exchange, speed reference, and emergency stop logic.
If your press has a PLC, look for a spooler with an analog or Modbus interface. That lets the press tell the spooler when to start, stop, and change speed. Without this handshake, operators must manually adjust the spooler, which defeats the purpose of high speed automation.
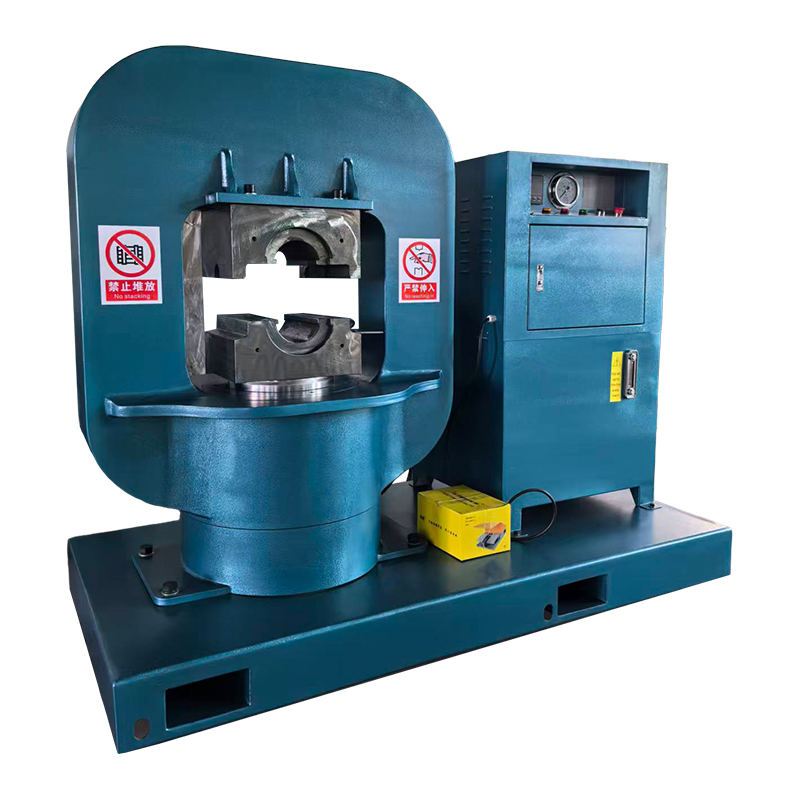 GT-1000 Hydraulic Wire Rope Sleeve Pressing Machine(Basket Frame)The hydraulic steel wire rope swage machine is equipped with a powerful two-stage hydraulic unit and has a safe design according to proven standards.View Product →
For example, a GT1000 basket frame press can be paired with a spooler that has a 0–10 V speed input. The press’s cycle start signal triggers the spooler to advance wire by a preset length. This simple integration reduces manual handling and improves safety.
Similarly, if you use an RDQ1010 annealing machine, the spooler must maintain tension even when the annealer stops for a torch change. A dancer-controlled spooler handles this gracefully because the loop keeps tension constant while the spooler pauses.
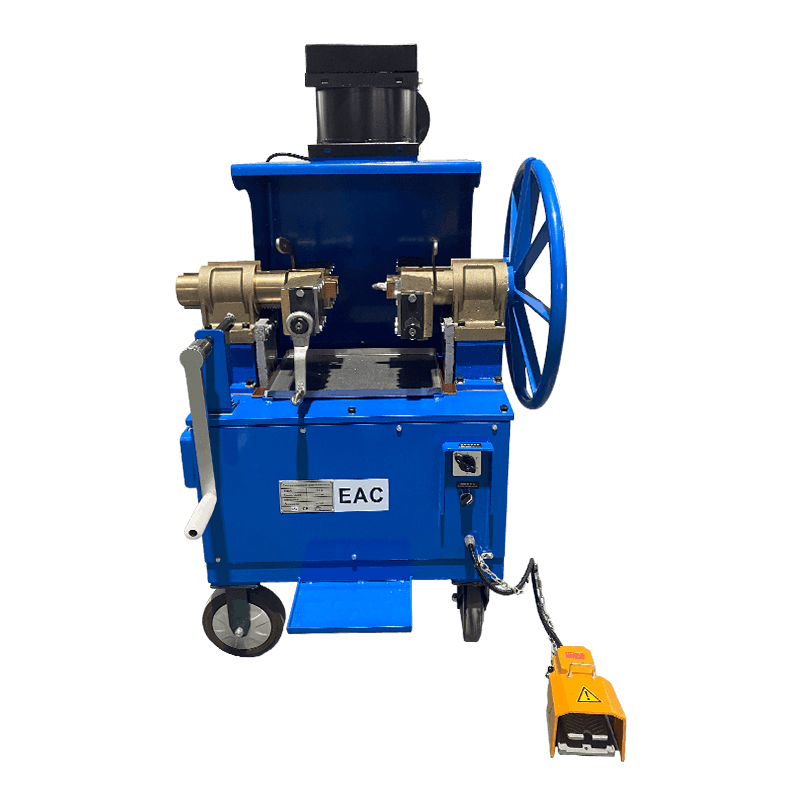
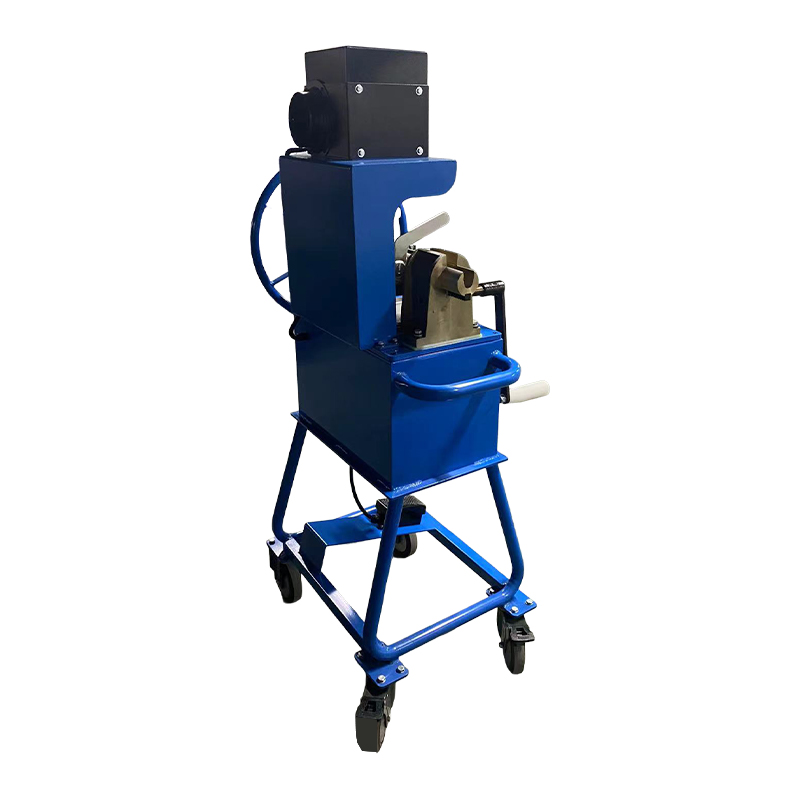 RDQ-1010 Steel Wire Rope Annealing MachineRDQ series steel wire rope cutting and tapering machines, with high melting speed and easy to operate, are applicable for melting steel ropes of various dimensions, es...View Product →
Visual Comparison: Spooling Speed vs. Wire Rope Diameter
The chart below shows a practical rule of thumb. It reflects typical recommendations from wire rope equipment manufacturers. Use it as a starting point, not a hard limit, because rope construction and press cycle time also matter.
These figures assume a powered payoff and a dancer-controlled take-up. For very stiff ropes or those with a high strand count, reduce the speed by 10–20%. The XT1600 spooler can be configured with different drum diameters to suit these ranges. Always confirm the maximum line speed with your rope supplier and press manufacturer.
Notice that the speed increase is not linear with diameter. Larger ropes need more time to bend around the drum, so tension control becomes more critical, not less. A machine that works well at 12 mm may struggle at 36 mm if the tension response is slow.
Maintenance and Safety Practices for High Speed Winding
A high speed spooler and coiler stores a lot of kinetic energy. Safety guards, emergency stops, and proper training are not optional. The same goes for maintenance: a bearing that fails at 200 m/min can send a drum flying.
Daily checks
- Inspect the wire rope path for sharp edges or worn guides.
- Check the air pressure if the spooler uses pneumatic brakes.
- Listen for unusual vibration or rubbing sounds.
Monthly maintenance
- Verify tension calibration with a known weight or a tension meter.
- Inspect the drum arbor and locking mechanism for wear.
- Clean the optical or proximity sensors that detect drum rotation.
Keep a spare set of guide rollers and a tension sensor on the shelf. Downtime costs more than parts. If you operate multiple shifts, consider a maintenance contract with your supplier to keep the spooler in top condition.
FAQ
What is a high speed spooler and coiler used for?
It is used to pay off and take up wire rope at controlled tension and speed. In a wire rope shop, it feeds hydraulic presses, annealing machines, and other processing equipment. It can also rewind rope for storage or shipping.
How do I choose the right line speed for my wire rope diameter?
Start with the chart above, but always test with your actual rope. Larger diameters generally run slower. The key is to maintain consistent tension; if the rope slips or birdnests, reduce speed until the problem disappears.
Can I use a spooler with an existing hydraulic press?
Yes, if the spooler has an interface that matches your press. Look for analog 0–10 V, 4–20 mA, or Modbus. A simple relay contact can start and stop the spooler, but for variable speed you need an analog or digital signal.
What maintenance does a high speed coiler need?
Daily visual checks, monthly tension calibration, and annual bearing replacement are typical. Keep the guide rollers clean and replace them when grooved. Always lock out power before servicing.
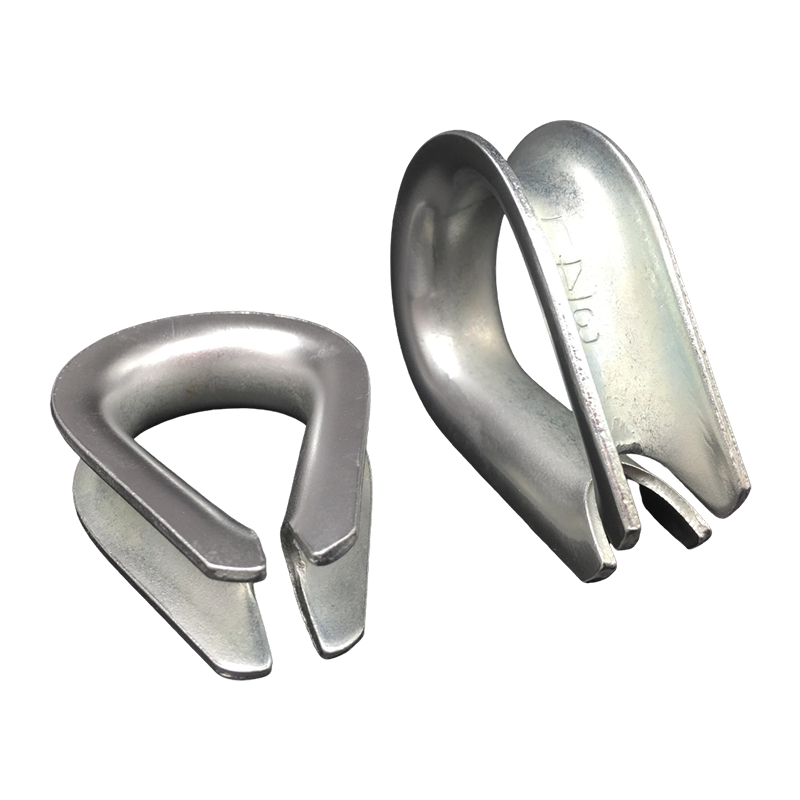
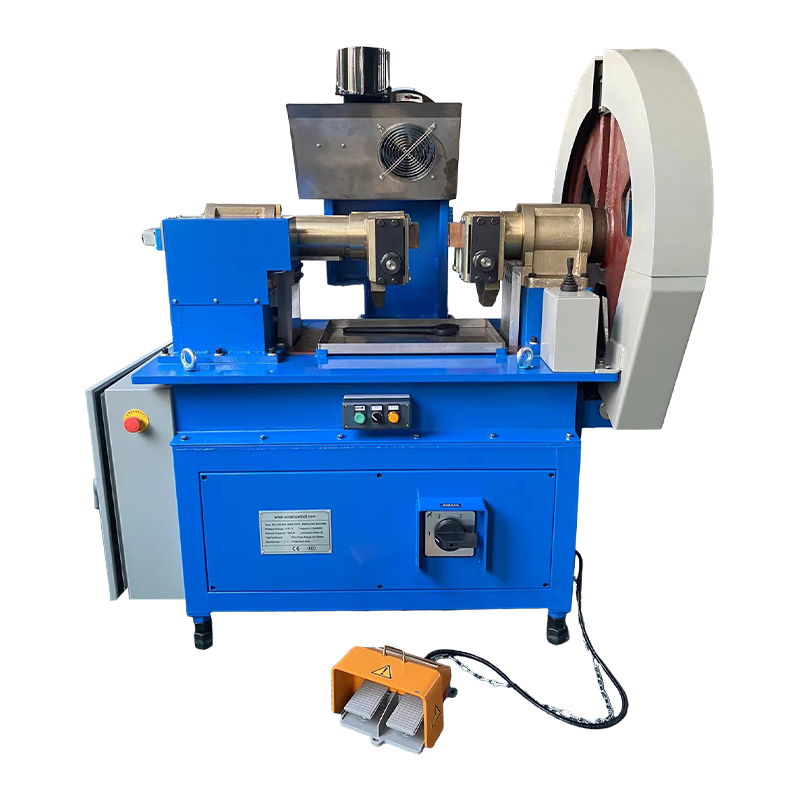
Jiangsu Xingtai Hydraulic Manufacturing Co., Ltd. has been building wire rope processing equipment since 1992. As a manufacturer and supplier, we offer hydraulic presses, annealing machines, reeling machines, and accessories such as aluminum ferrules and thimbles. Our XT1600 spooler and coiler is designed for high speed, stable tension, and easy integration with existing lines. If you need a wholesaler for a complete wire rope workshop, we can help you select the right combination.
For more details on how reeling machines fit into wire rope production, see our industry article: what is a wire rope rolling machine used for.
If you require custom hydraulic equipment or technical consultation, please feel free to contact the Xingtai Sales and Engineering Team.
-
 +86-523-86934677
+86-15896002505 -
 [email protected]
-
 +86-15896002505
-
 No. 3 Longgang Road, Gaogang Port Street, Taizhou City, China.
Copyright © Jiangsu Xingtai Hydraulic Manufacturing Co., Ltd. All Rights Reserved. Custom hydraulic machinery manufacturers Wholesale wire rope swagers Factory