 English
 русский
 Français
 Español
 Português
 Deutsch
 عربى
 Türk
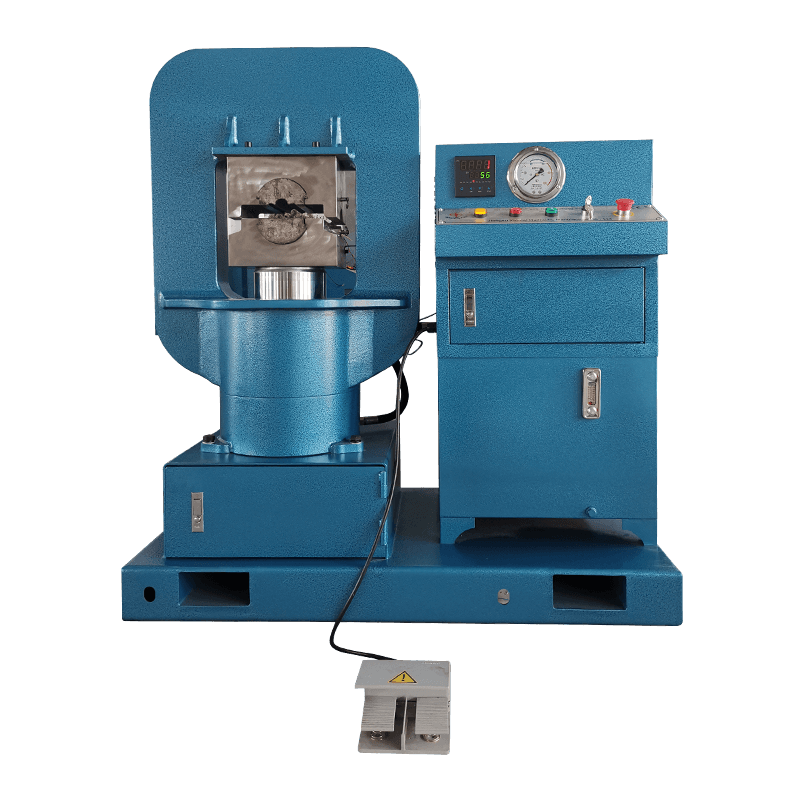
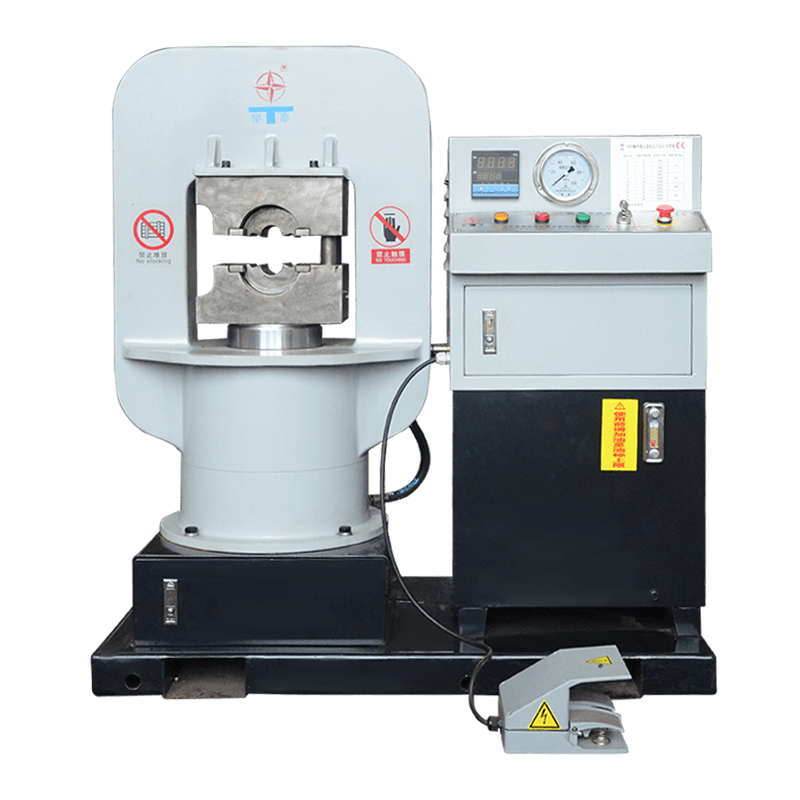
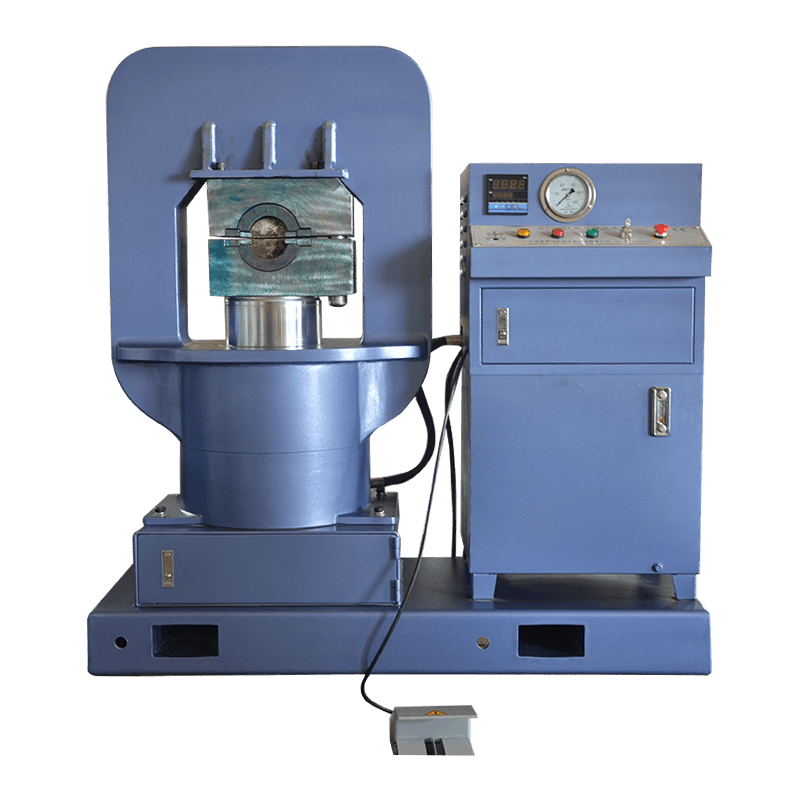
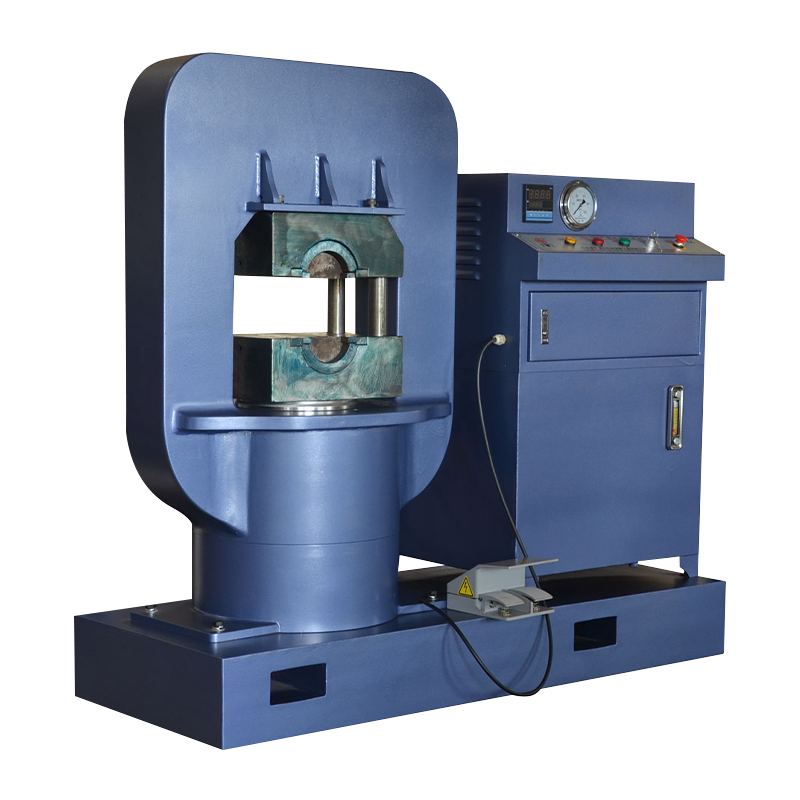
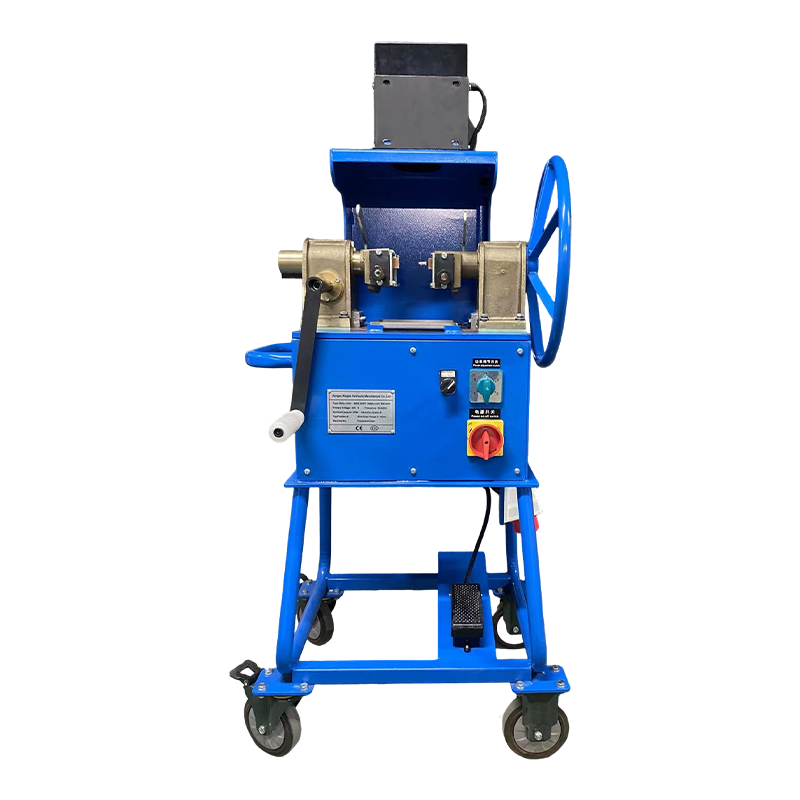
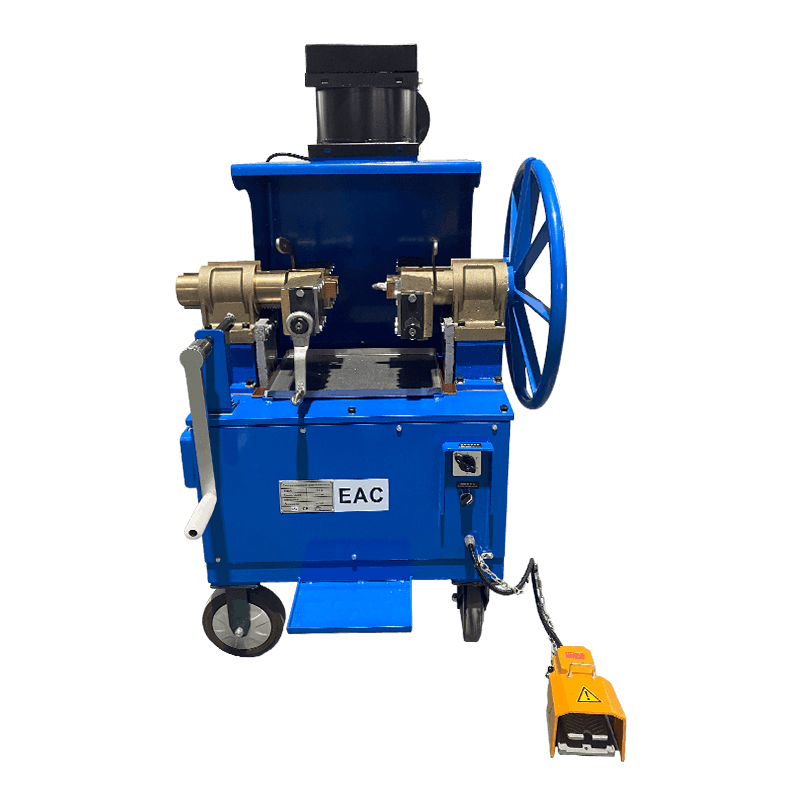
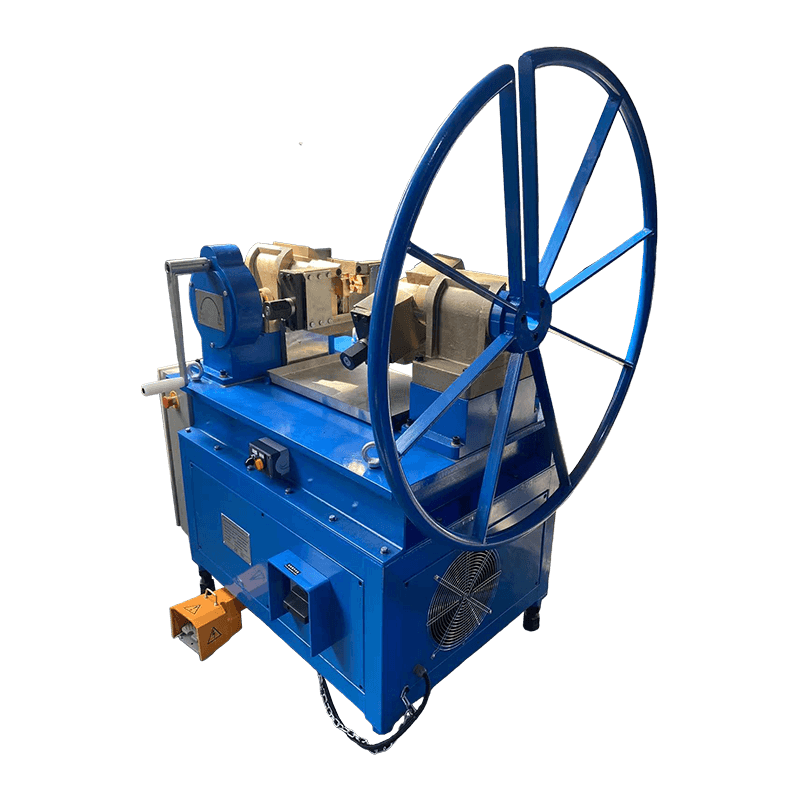
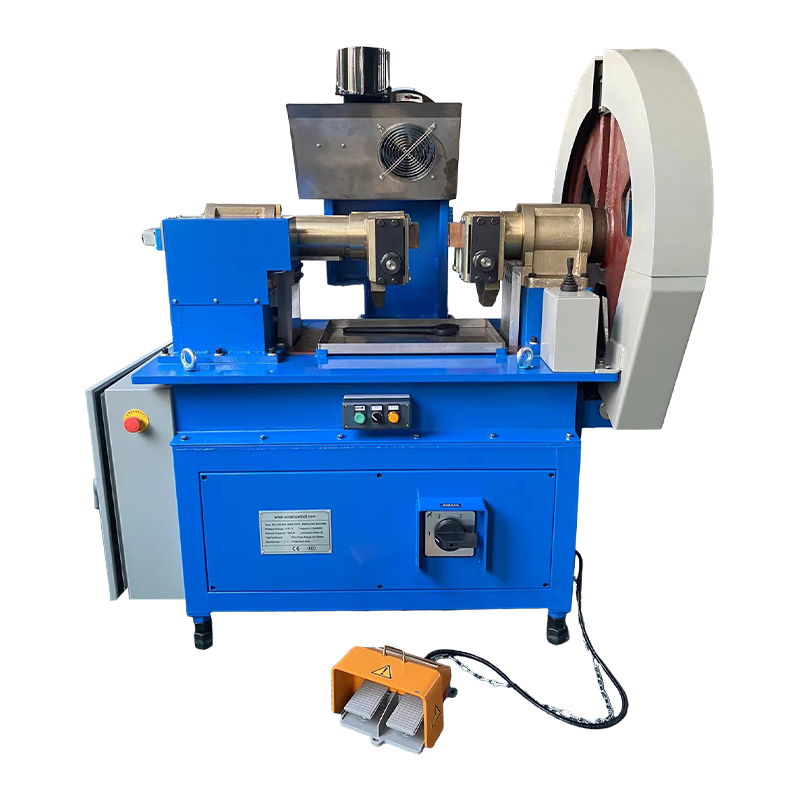
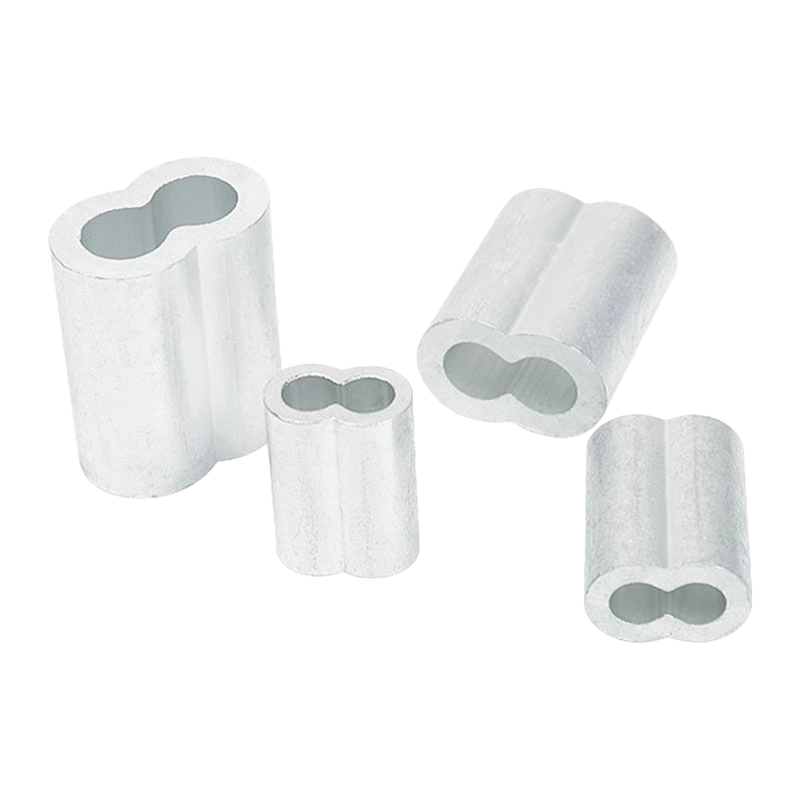
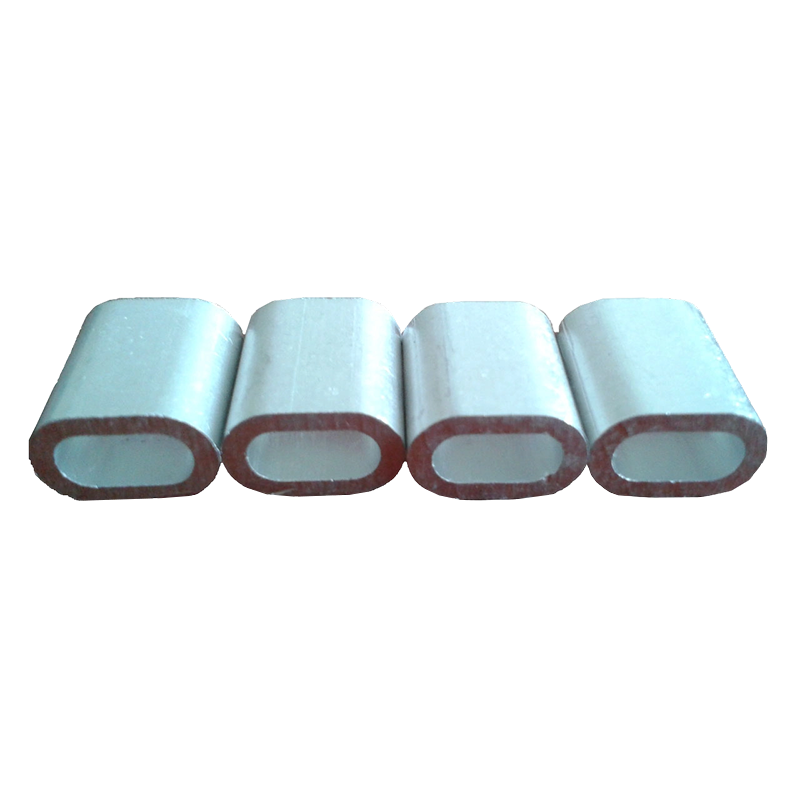
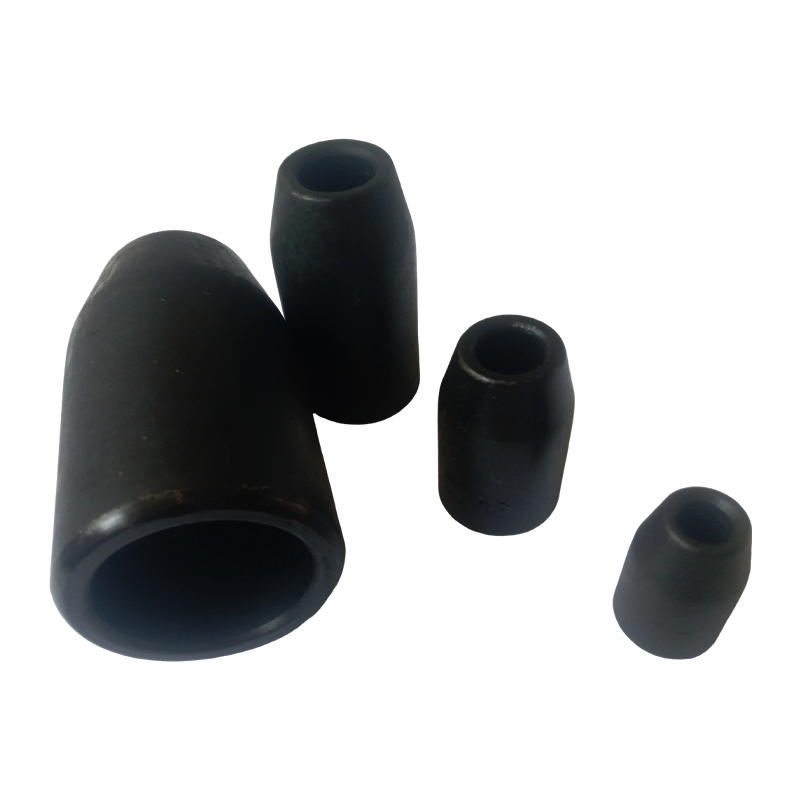
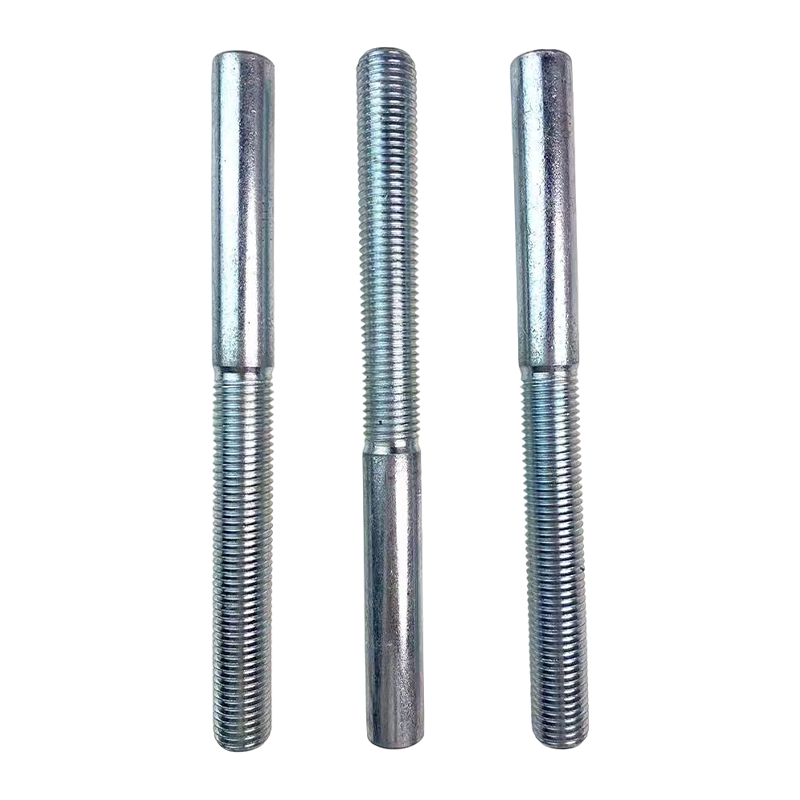
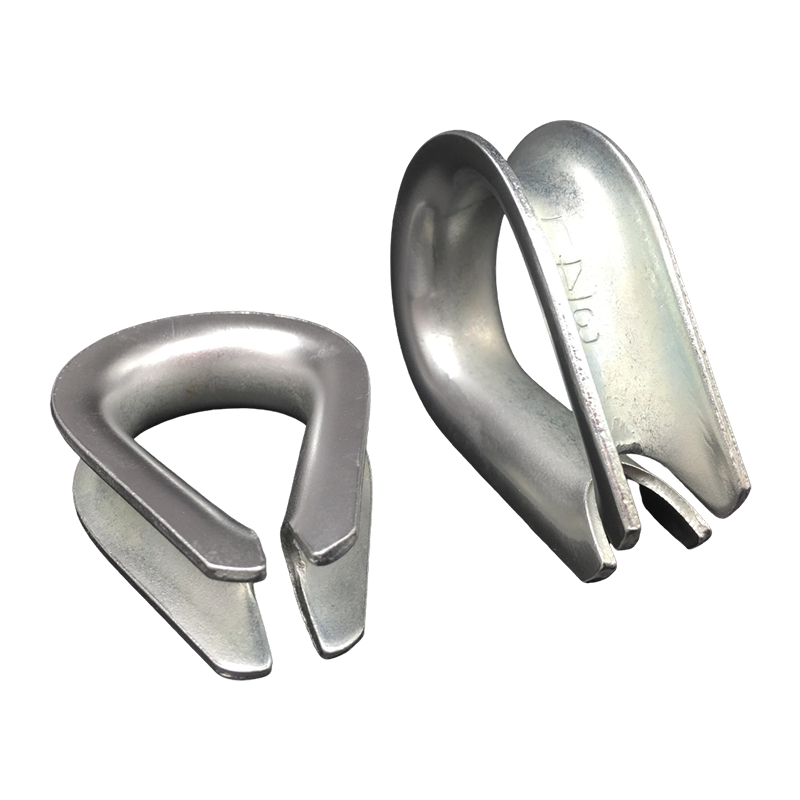
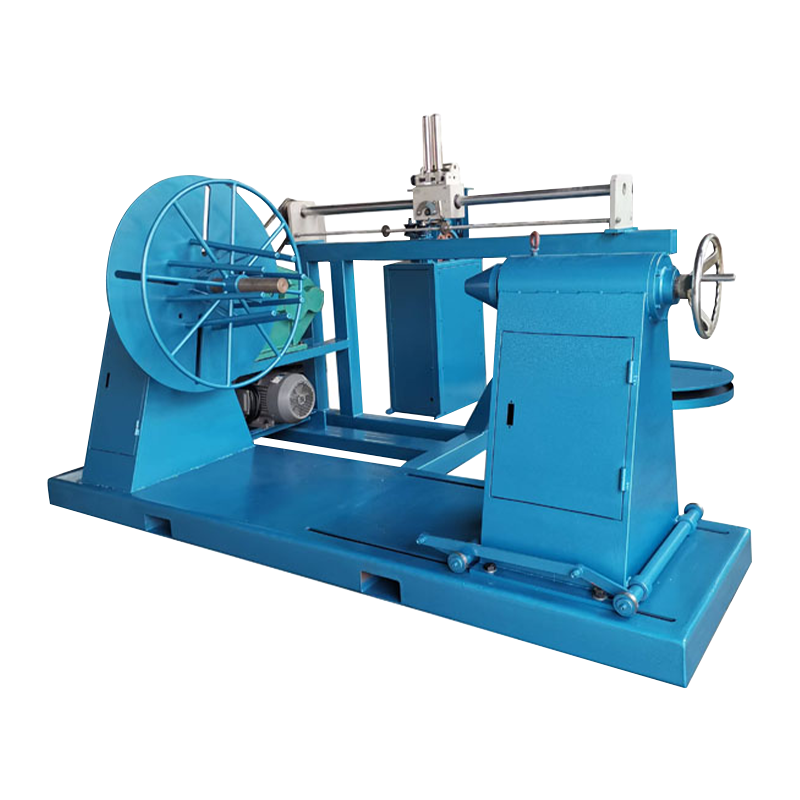
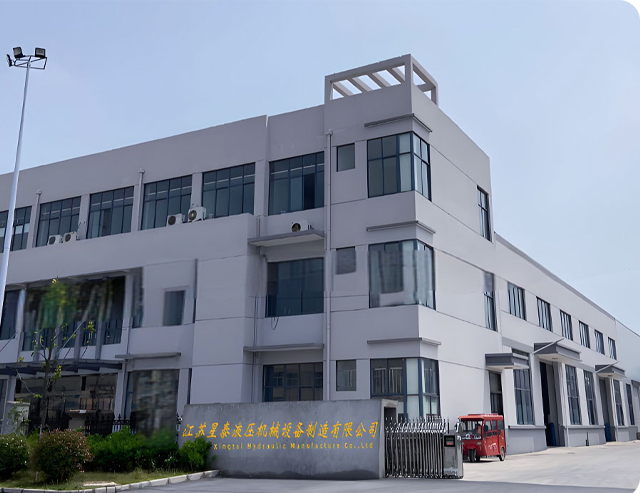
As Wire Rope & Rigging Industry Suppliers and Wire Rope & Rigging Industry Factory, Jiangsu Xingtai Hydraulic Manufacturing Co., Ltd. was founded in 1992 and is located in Taizhou City, Jiangsu Province, China. The company specializes in manufacturing hydraulic wire rope pressing machines, wire rope annealing and tapering machines, aluminum sleeves, and lifting clamps. Xingtai Hydraulic is equipped with advanced production facilities, strong technical capabilities, authoritative testing equipment, and a comprehensive quality management system.
The swaging components of Xingtai Hydraulic machines are forged from high-strength alloy steel. The machine body is manufactured from a single block of material, ensuring structural integrity and long service life. Our hydraulic systems utilize a dual-pressure pump oil supply system, which enables fast upward and downward movement while ensuring a smooth pressing process. This design significantly improves pressing quality and production efficiency.
Xingtai Hydraulic machines have been exported to numerous countries, including the UK, Australia, the Netherlands, Latvia, Malaysia, Thailand, India, Russia, Botswana, Poland, and others.
Guided by the philosophy of "high quality, competitive price, and lasting commitment," we strive to meet our customers' needs and provide them with the best service. We remain dedicated to serving both existing and new clients with the same level of excellence as we work together to build a successful future.
SEARCH
CATEGORY
Wire Rope & Rigging Industry Suppliers
Company
Jiangsu Xingtai Hydraulic Manufacturing Co., Ltd.
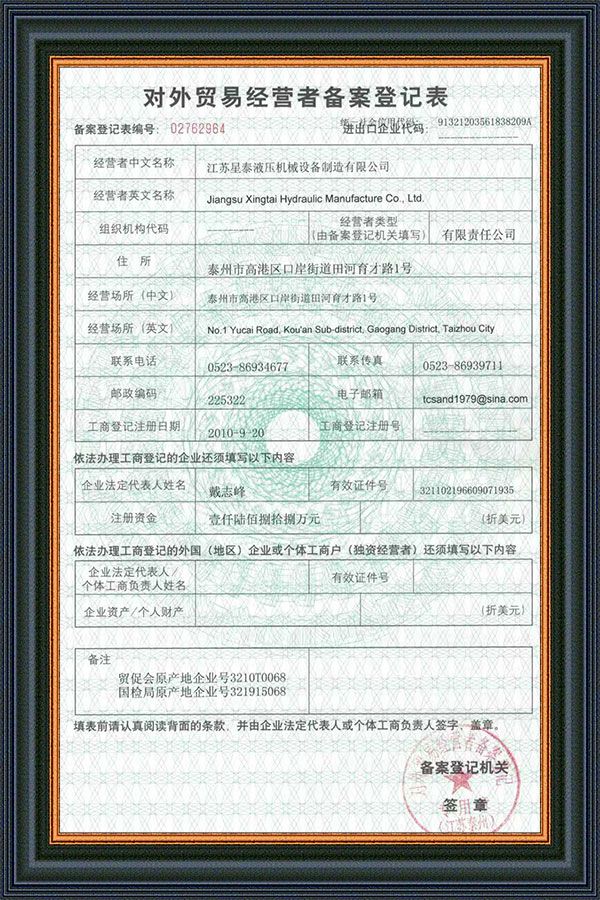
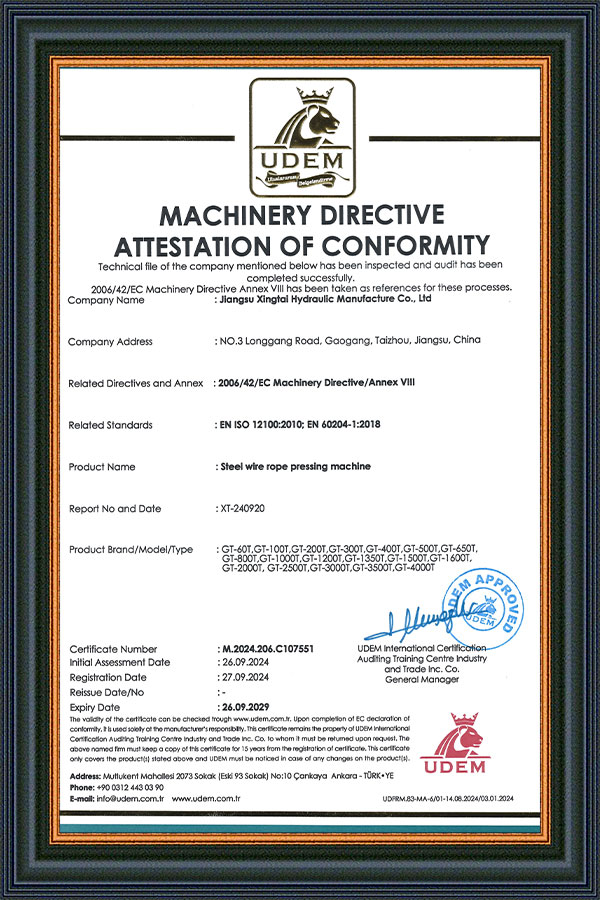
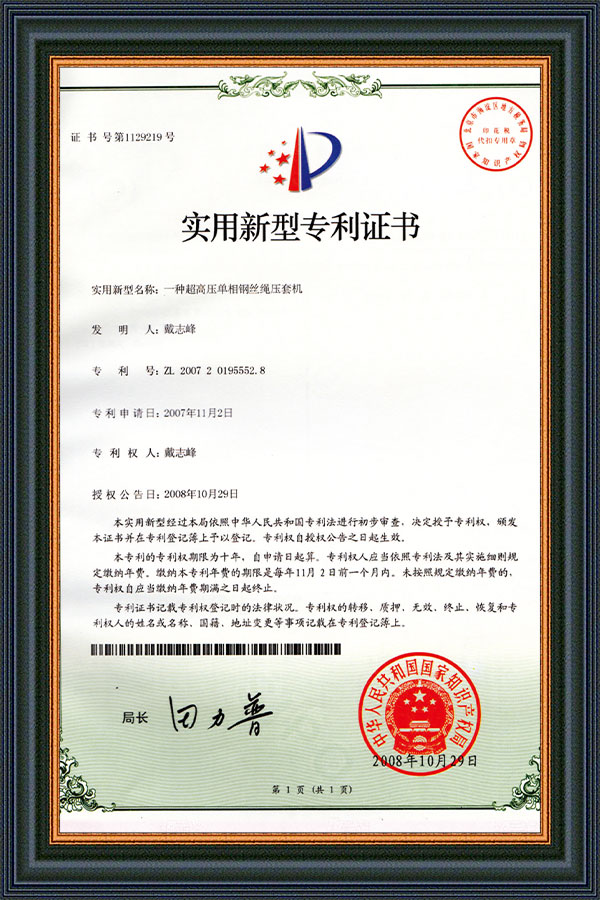
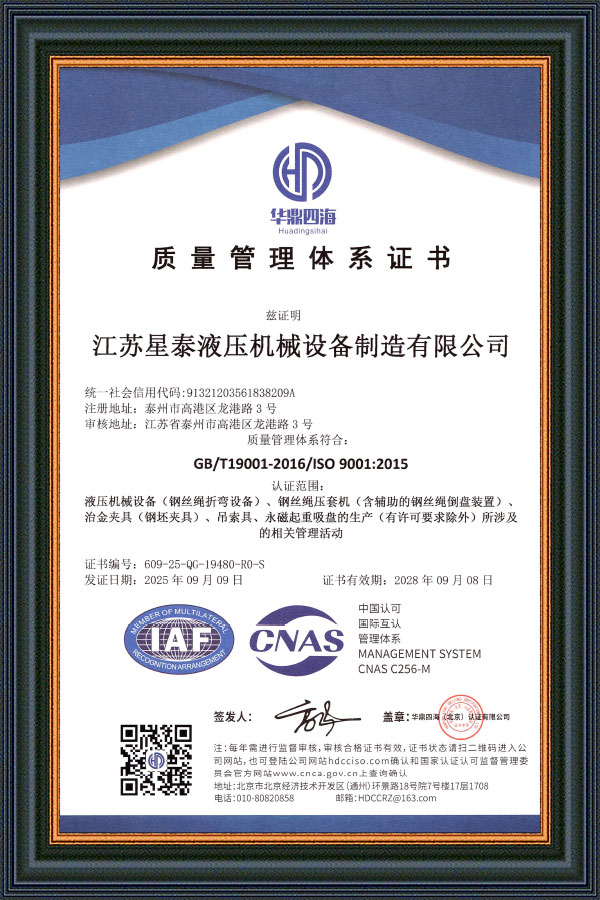
Certificate
News
-
A fitter checks a cable with a caliper, gets 5.8 mm across the outer jacket, and asks whether the conductor is 10 AWG. That reading is not a wire gauge yet. The jacket, the air gap under the jacket, ...
READ MORE -
How Do You Measure Wire Gauge? The Direct Answer To answer how do you measure wire gauge, start with the metal, not the plastic: strip a short section of insulation and measure the bare conductor wit...
READ MORE -
Aluminium Hourglass Sleeves and Wire Rope Terminations: What Buyers Should Confirm First A wire rope termination can look correct on the bench and still cause trouble in service if the sleeve, the ro...
READ MORE -
When you are setting up a wire rope processing line, the high speed spooler and coiler often becomes the bottleneck or the hero. A spooler that runs smoothly at 200 meters per minute can keep your hy...
READ MORE -
When a 12-ton cable reel stalls halfway through a tunnel pull, the cost is rarely just the roller that failed. The crew stops, the winch cools down, the cable jacket may already be scarred, and the s...
READ MORE
Industry Knowledge
What Is the Safest Way to Inspect Wire Rope Before Use? A Complete Guide to Wire Rope Inspection
In the wire rope & rigging industry, a single overlooked defect can lead to catastrophic failure. Studies show that over 40% of wire rope failures are directly attributable to inadequate pre-use inspection. Whether you are working with galvanized vs stainless steel wire rope, understanding the correct inspection procedure — combined with a reliable wire rope inspection checklist — is the foundation of worksite safety and regulatory compliance.
1. Why Pre-Use Inspection Is Critical in the Wire Rope & Rigging Industry
Wire rope degrades through corrosion, fatigue, mechanical abuse, and improper storage. OSHA 1910.184 mandates that wire rope used in rigging must be inspected before each use. Failure to do so not only violates regulations but puts lives at risk. The wire rope working load limit chart provided by the manufacturer assumes the rope is in serviceable condition — a damaged rope may retain only 30–50% of its rated capacity.
Primary Causes of Wire Rope Failure (%)
Fatigue & Cyclic Loading
38%
Corrosion (esp. in marine environments)
27%
Mechanical Abuse / Kinking
20%
Improper Storage / Handling
15%
Fig. 1 — Distribution of wire rope failure causes. Fatigue and corrosion together account for over 65% of all failures.
2. Step-by-Step Wire Rope Inspection Checklist
A thorough wire rope inspection checklist should cover visual, tactile, and dimensional assessments. Follow these steps before every lift or rigging operation:
(1) Visual Surface Inspection
Run the rope through a clean cloth and scan for broken wires, rust staining, kinks, bird-caging, or crush damage. ASME B30.9 states that a rope must be removed from service if 6 or more broken wires are found in one rope lay, or 3 or more broken wires in one strand.
(2) Diameter Measurement
Use calibrated calipers to measure rope diameter at multiple points. A reduction in diameter of more than 3% from the nominal size indicates internal wear or core failure and warrants immediate retirement of the rope.
(3) Corrosion Assessment — Galvanized vs Stainless Steel Wire Rope
Understanding the difference between galvanized vs stainless steel wire rope is essential here. Galvanized rope may show white zinc corrosion before red rust appears — both are warning signs. Stainless steel (316-grade) is significantly more resistant but should still be checked for pitting or crevice corrosion at end fittings.
(4) End Termination and Fitting Check
Swaged ferrules, wedge sockets, and wire rope clips are common failure initiation points. Inspect for cracks, deformation, or slippage. Improperly applied U-bolt clips can reduce rope efficiency to as low as 80% of rated capacity.
(5) Lubrication Check
Dry or cracking outer surfaces indicate lubricant depletion. A properly lubricated wire rope can extend service life by up to 200% compared to an unlubricated rope under the same conditions.
| Inspection Item | Method | Discard Threshold | Reference Standard |
|---|---|---|---|
| Broken wires | Visual / tactile | ≥6 in one lay / ≥3 in one strand | ASME B30.9 |
| Diameter reduction | Caliper measurement | >3% of nominal | ISO 4309 |
| Corrosion (surface) | Visual inspection | Deep pitting or flaking | OSHA 1910.184 |
| Kinking / deformation | Visual inspection | Any permanent kink | ASME B30.9 |
| End fitting integrity | Visual / torque check | Any crack or deformation | EN 13411 |
3. Understanding the Wire Rope Working Load Limit Chart
The wire rope working load limit chart (WLL) defines the maximum load a rope should carry under normal service conditions, typically calculated as the Minimum Breaking Load (MBL) divided by a safety factor — commonly 5:1 for overhead lifting and 3.5:1 for non-critical applications. Always verify the WLL against the actual load before use.
Approximate Working Load Limit (WLL) by Rope Diameter — 6×19 IWRC, 5:1 Safety Factor (tonnes)
Fig. 2 — Wire rope working load limit chart for 6×19 IWRC construction at 5:1 safety factor. Always consult manufacturer data for your specific rope construction.
4. Galvanized vs Stainless Steel Wire Rope — Which Is Safer for Your Application?
Choosing the right material is as important as the inspection process itself. In the wire rope & rigging industry, the two dominant materials each have distinct strengths:
- Galvanized wire rope — zinc coating provides sacrificial corrosion protection. Cost-effective for construction, mining, and suspension bridge applications. Zinc layer typically lasts 10–25 years depending on environment.
- Stainless steel wire rope (316-grade) — superior corrosion resistance in marine, food-grade, and architectural environments. Higher initial cost but lower lifecycle maintenance. Tensile strength range of 1,000–1,570 MPa for drawn grades.
- In salt-spray testing, 316 stainless steel wire rope shows no significant corrosion after 1,000+ hours, while ungalvanized carbon steel begins to show red rust within 72 hours.
Galvanized vs Stainless Steel Wire Rope — Performance Comparison (Score 1–10)
Fig. 3 — Radar comparison: galvanized vs stainless steel wire rope across five performance dimensions.
5. How Inspection Frequency Affects Service Life
Data from crane operators in the wire rope & rigging industry shows that ropes inspected at regular monthly intervals have a service life 35–50% longer than those inspected only annually. The line chart below illustrates the relationship between inspection frequency and cumulative failure rate over a 5-year period.
Cumulative Wire Rope Failure Rate (%) by Inspection Frequency Over 5 Years
Fig. 4 — Cumulative failure rate over 5 years by inspection frequency. Monthly inspection dramatically reduces risk over time.
Stay in touch with Xingtai.
If you require custom hydraulic equipment or technical consultation, please feel free to contact the Xingtai Sales and Engineering Team.
Quick Links
Product Category
Contact Us
-
 +86-523-86934677
+86-15896002505 -
 [email protected]
-
 +86-15896002505
-
 No. 3 Longgang Road, Gaogang Port Street, Taizhou City, China.
Copyright © Jiangsu Xingtai Hydraulic Manufacturing Co., Ltd. All Rights Reserved. Custom Wire Rope & Rigging Industry Suppliers Wholesale wire rope swagers Factory

